Dehumidifier for Automotive Manufacturing
Engineered for automotive manufacturing, our dehumidifiers provide precise humidity control to reduce condensation, corrosion, coating defects, and moisture-related production risks.
With energy-efficient operation, flexible installation, smart controls, and OEM customization, they maintain stable conditions across assembly, painting, storage, and testing.
Why Moisture Control Matters in Automotive Manufacturing
Condensation Control
Reduce condensation on metal components, equipment, molds, surfaces, and stored automotive parts.
Corrosion Prevention
Protect steel components, tools, molds, and finished parts from moisture-related corrosion.
Paint & Coating Quality
Control humidity during painting and coating to support adhesion, drying, surface finish, and quality.
Stable Production Conditions
Maintain consistent humidity for automotive assembly, inspection, testing, and quality control.
Automotive Dehumidifier Solutions
Our automotive dehumidifiers offer flexible configurations for production, testing, storage, and other controlled automotive environments.
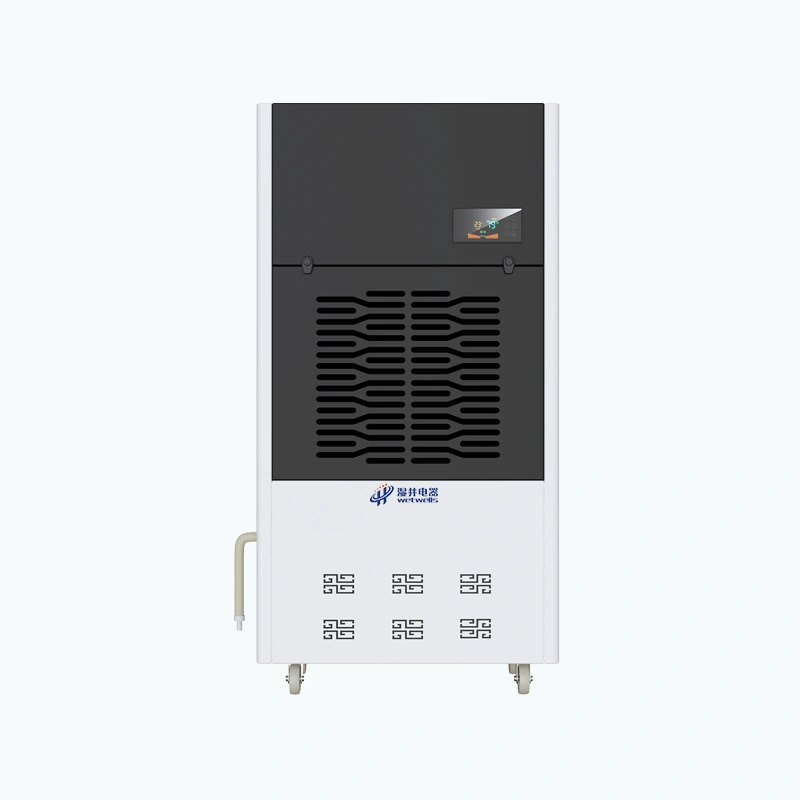
Refrigerant Dehumidifier
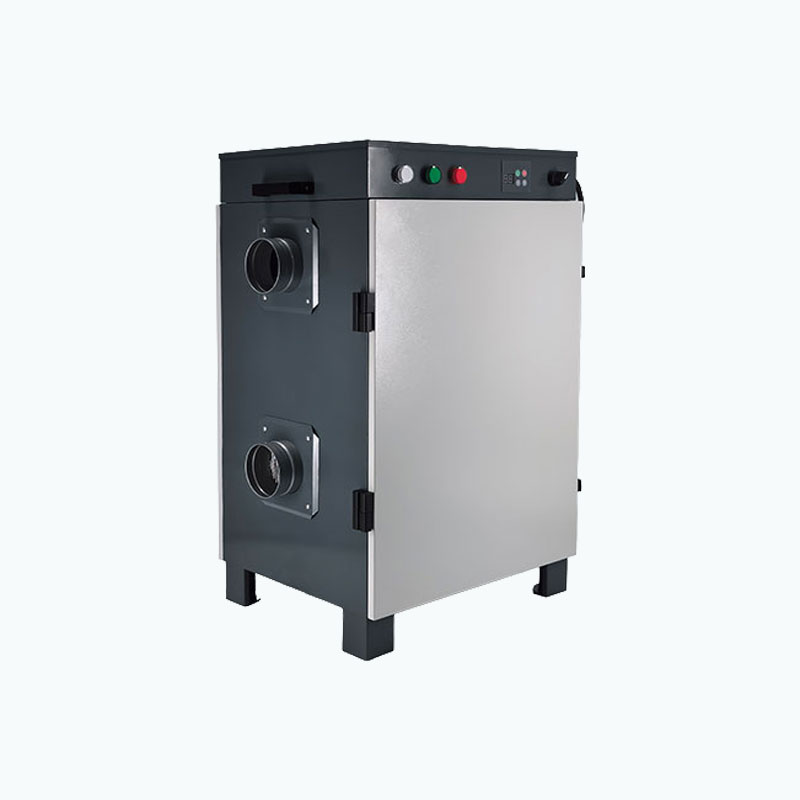
Desiccant Dehumidifier
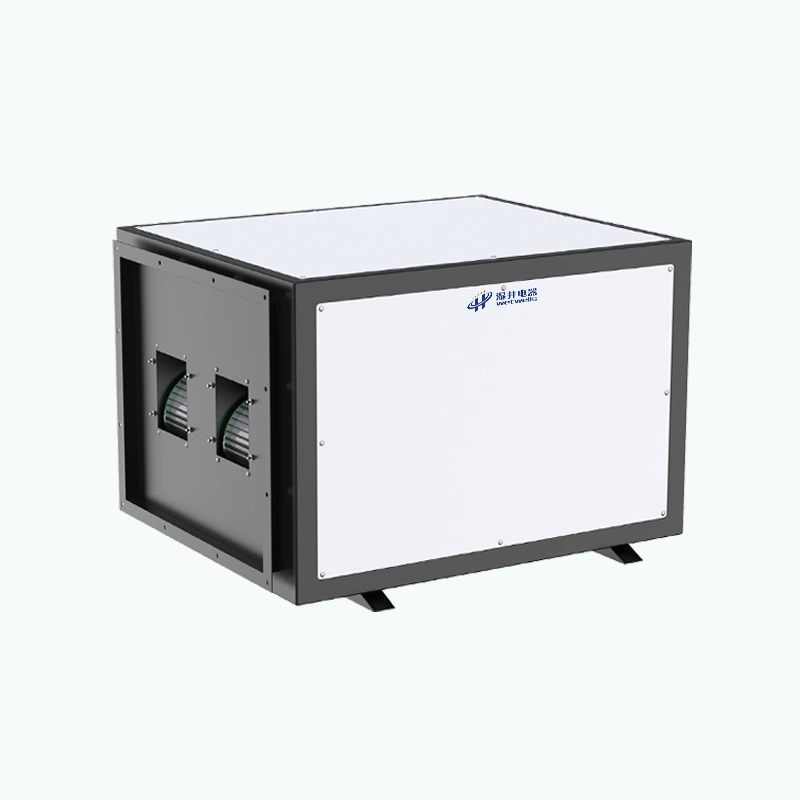
Ducted Dehumidifier
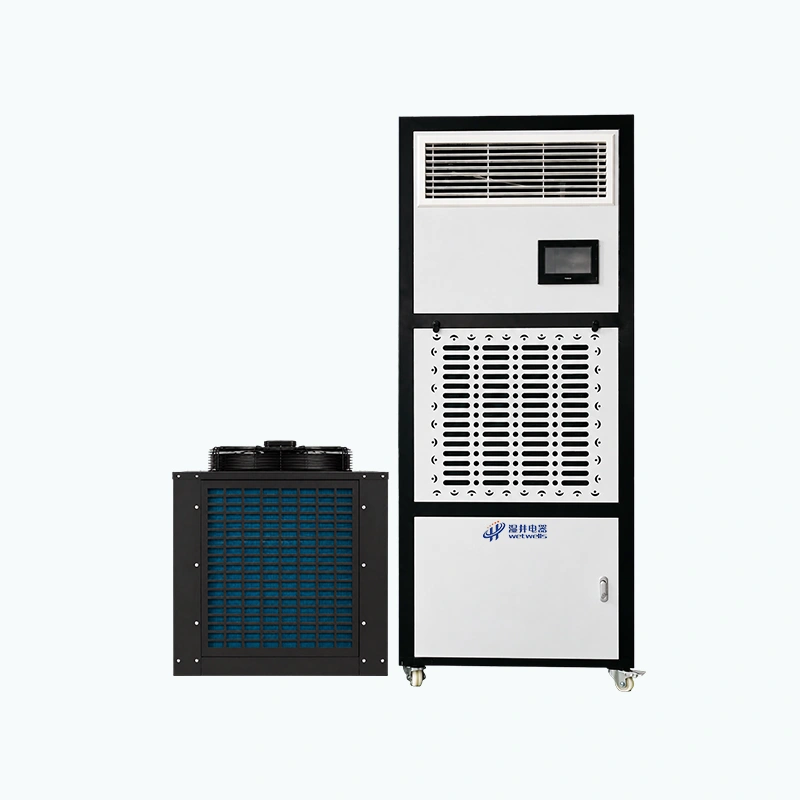
Constant Temperature & Humidity Unit
Dehumidification Requirements for Automotive Manufacturing
Different automotive processes require specific humidity and temperature conditions. Proper dehumidification protects components, reduces corrosion, and supports stable production quality.
Not Sure Which Dehumidifier Fits Your Factory?
Share your application details, including room size, temperature, current humidity, target RH, and operating conditions. Our team will help calculate the required capacity and recommend the optimal configuration.
Automotive Industry Dehumidification Project
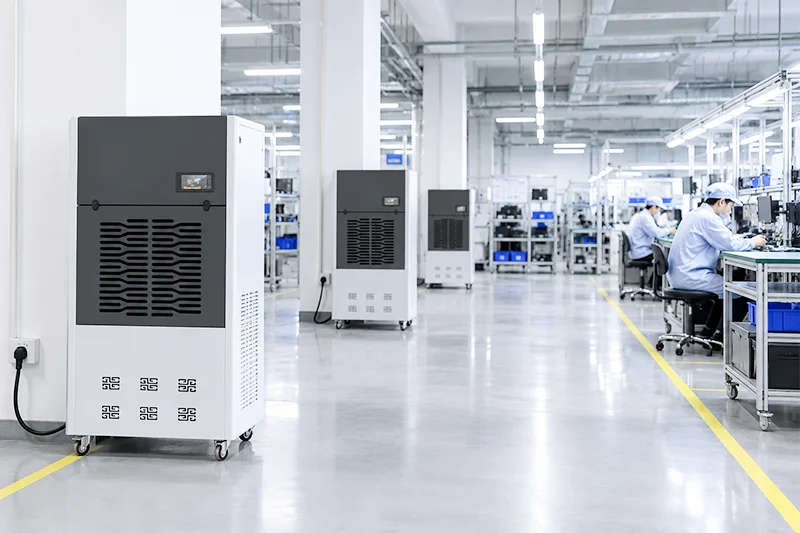
An automotive electronics manufacturer needed stable humidity control in its assembly and inspection area, where outdoor humidity and fresh-air intake caused frequent RH fluctuations.
Project Requirements
Our Solution
The project used 3 industrial dehumidifiers, each rated at 240 L/day with 3,000 m³/h airflow, providing a total capacity of 720 L/day and 9,000 m³/h airflow.
The units included automatic humidity control, continuous drainage, defrost, power-off memory, and RS485 communication.
Project Result
The system maintained the controlled area at approximately 45%–55% RH, reducing humidity fluctuations and supporting stable conditions for assembly, inspection, testing, and quality control.