Dehumidifier for Pharmaceutical Industry
We provide pharmaceutical dehumidification solutions with precise humidity control for cleanrooms, production areas, laboratories, and storage environments.
Our dehumidifiers help reduce moisture-related risks, protect pharmaceutical materials and products, and support stable GMP-controlled manufacturing environments.
What Pharmaceutical Environments Require Dehumidification?
We deliver reliable humidity control solutions for pharmaceutical facilities to protect products, materials, and production processes.
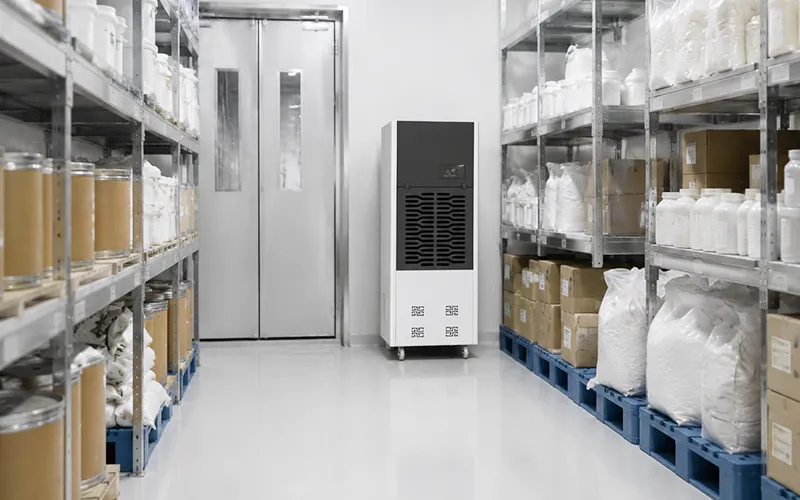
Raw Material Storage
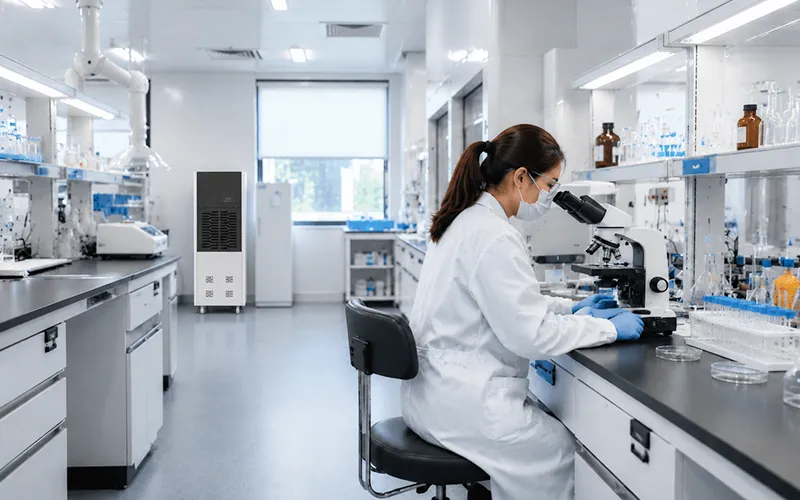
R&D Laboratory
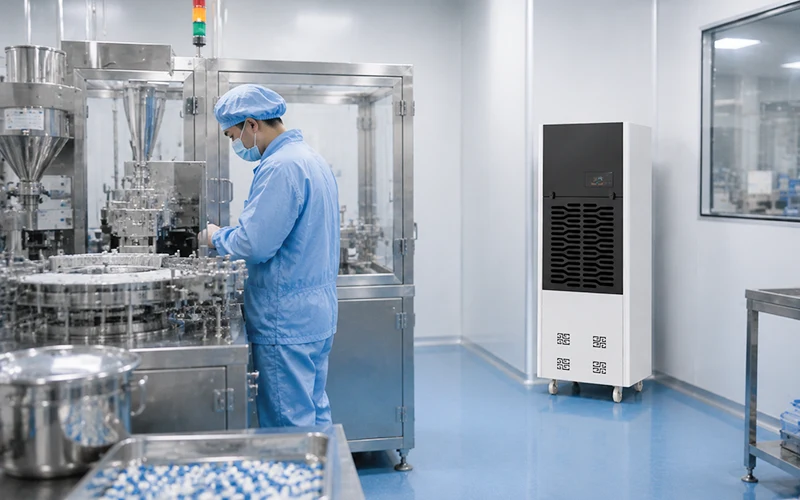
Tablet & Capsule Production Room
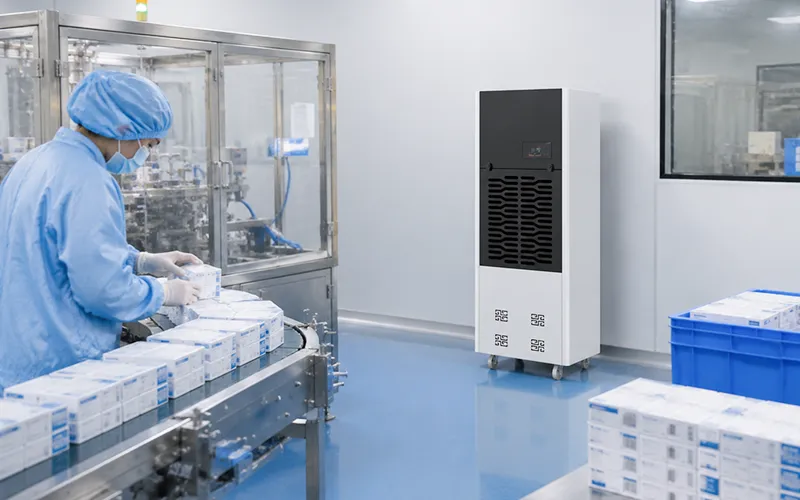
Packaging Room
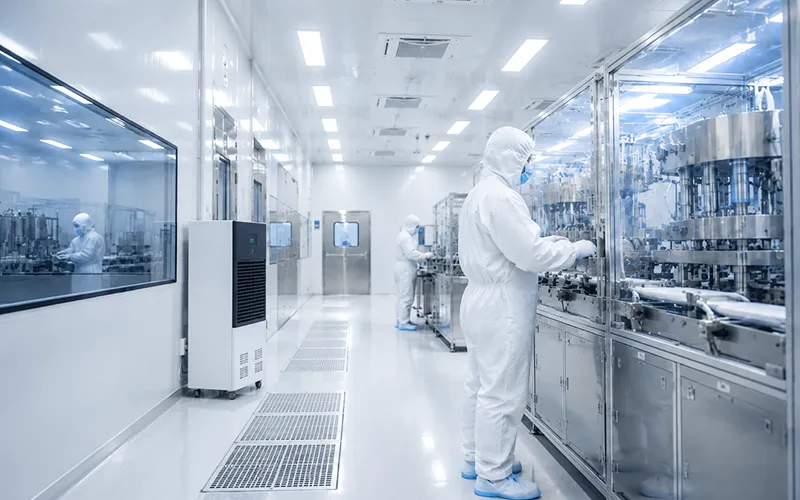
Cleanroom
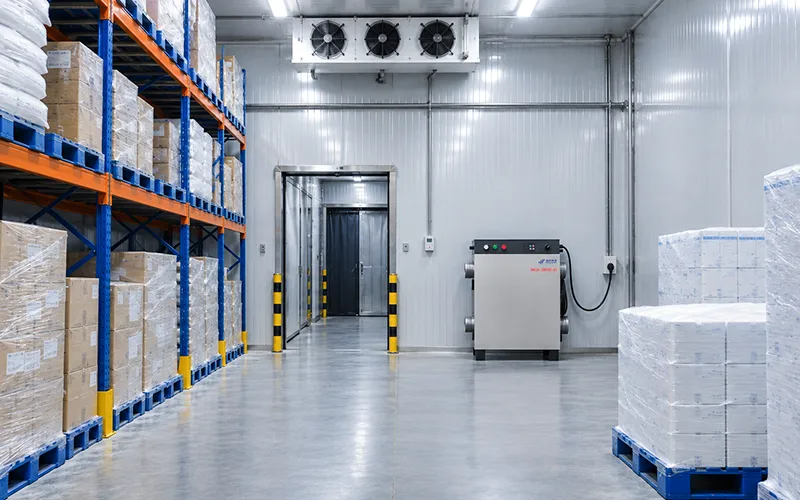
Cold Storage
What Pharmaceutical Products Require Precise Humidity Control?
Different pharmaceutical products require specific humidity conditions. Our dehumidifiers provide reliable moisture control to protect drug quality and stability.
Antibiotic Medications
Prevent powder clumping caused by excessive moisture, ensuring stable solubility, activity, and drug quality.
Biologics
Maintain strict humidity control to protect protein structures and preserve the stability and effectiveness of biological products.
Cardiovascular Drugs
Control moisture levels to maintain dissolution performance, drug stability, and consistent therapeutic effectiveness.
Gastrointestinal Medications
Prevent moisture-related powder clumping and degradation to maintain drug efficacy and product quality.
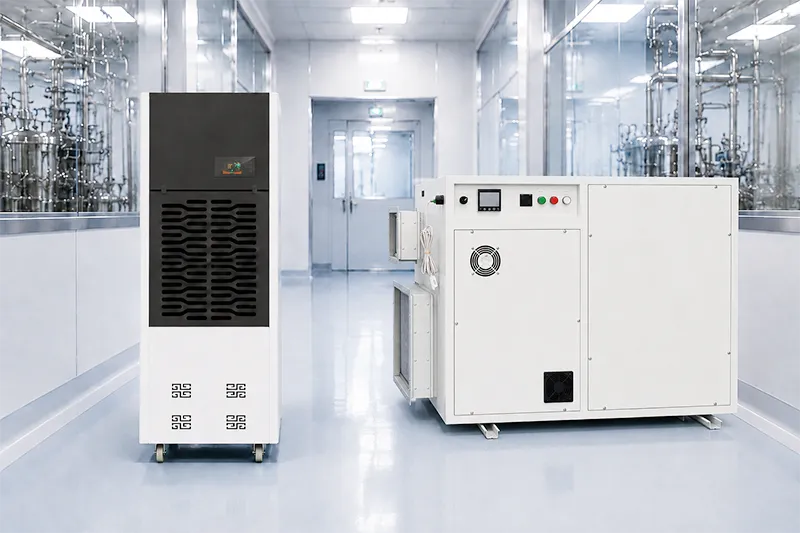
Refrigerant vs. Desiccant Pharmaceutical Dehumidifier
Airflow Configuration Options
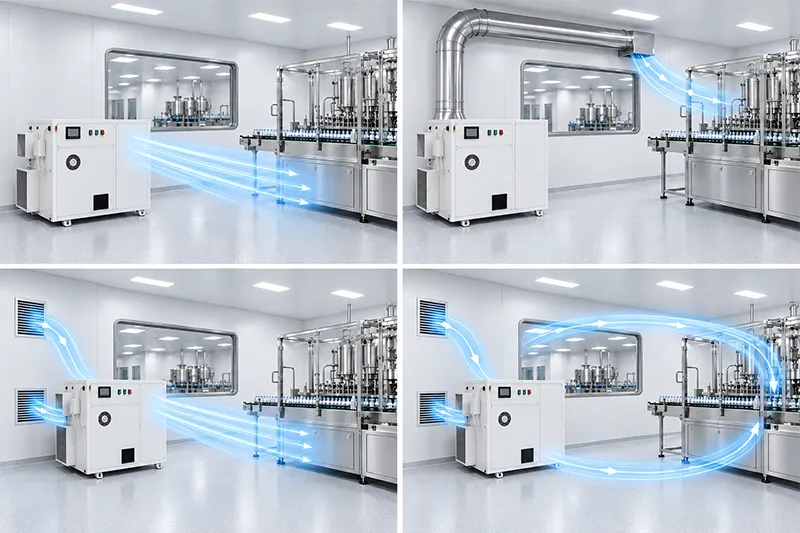
We offer flexible airflow configurations to match pharmaceutical cleanrooms, production areas, ventilation requirements, and HVAC integration needs.
Customize Your Pharmaceutical Dehumidification Solution
From humidity control and airflow design to filtration and system integration, we provide complete solutions for pharmaceutical manufacturing environments.
Why Choose Our Pharmaceutical Dehumidifier?
Integrated Climate Control System
Combines dehumidification, heating, cooling, and HEPA H13 filtration for a stable pharmaceutical environment.
High Airflow Capacity
Provides up to 14,000 m³/h airflow for large pharmaceutical production areas.
Advanced Air Purification System
HEPA H13 filtration removes 99.95% of 0.3 μm particles to support GMP requirements.
Durable Outdoor Protection Design
Weather-resistant and corrosion-resistant design enables reliable outdoor installation.