Select semiconductor humidity systems by defining process-specific moisture limits, calculating loads, and matching dehumidification, humidification, and monitoring to production zones. The design may combine facility air treatment with dedicated dry enclosures.
Verify equipment ratings under project conditions, then confirm contamination protection, control stability, and performance through commissioning before production acceptance.
Define Humidity Requirements Around the Process
Identify Which Areas Actually Need Tight Control
Photolithography, coating, metrology, wafer handling, and packaging can respond differently to moisture fluctuations. Treating every production space identically may waste conditioning capacity while overlooking sensitive operations.
Start with specifications from process owners, tool suppliers, material handlers, and quality teams. Distinguish environmental conditions needed for operation from tighter limits established for measurement repeatability or product handling.
Record the reason behind each limit and the consequence of exceeding it. This information guides zoning decisions, alarm priorities, and discussions about backup capacity.
A cleanroom controls airborne contamination through its design and operation, but its particle classification alone does not prescribe a universal semiconductor humidity band. Temperature and moisture requirements must be specified separately.
Write Measurable Limits Rather Than One Setpoint
An actionable requirement defines the permitted humidity band, spatial uniformity, time stability, excursion duration, and recovery after disturbance. It also identifies where compliance must be demonstrated.
Separate operating targets from warning alarms, intervention limits, and shutdown responses. A momentary door-opening excursion may require different action from persistent drift during critical exposure.
Specify averaging periods and sampling frequency before writing acceptance criteria. A slow trend display can conceal short disturbances that matter to a sensitive process.
Record temperature alongside relative humidity (RH). RH changes when temperature changes, even without additional water vapor, so temperature excursions can masquerade as moisture-control failures.
Separate Room Conditions From Dry Tools and Gases
A dry cabinet, mini-environment, or tool enclosure may require much lower moisture content than the surrounding room. Specify its internal condition independently of ambient RH.
For nitrogen or compressed process gases, request dew-point or frost-point conditions and their measurement pressure. A gas specification cannot be transferred directly into a room-RH requirement.
Pressure changes alter how gas moisture readings are interpreted. Confirm whether specifications refer to line pressure, atmospheric pressure, or a defined sampling arrangement.
| Controlled location | Primary specification | Essential acceptance evidence |
| Production bay | RH and temperature across occupied process locations | Mapped uniformity and trend stability |
| Metrology room | Conditions at instruments and measurement intervals | Local records during representative work |
| Dry cabinet or enclosure | Internal moisture level and recovery after access | Logged recovery at product positions |
| Process gas supply | Dew/frost point at stated pressure and sampling point | Calibrated sample-line measurement |
Calculate Moisture Loads Before Sizing Equipment
Distinguish Makeup Air From Recirculated Air
Outdoor makeup air often creates a major latent load, especially when humid air replaces exhausted process air. Calculate its water-vapor contribution at relevant seasonal design conditions.
Recirculated air can carry substantial airflow without importing equivalent outdoor moisture. Avoid multiplying full recirculation volume by outdoor humidity difference when estimating dehumidifier capacity.
Review exhaust schedules, pressure offsets, door traffic, personnel, cleaning, open water processes, and infiltration. Each changes the moisture balance differently during production and maintenance.
Examine Existing Air Treatment and Part-Load Operation
Document makeup-air units, air-handling units, cooling coils, reheat, supply conditions, and available utility capacities. Confirm whether existing equipment already removes enough moisture at demanding conditions.
Check performance during startup, reduced production, filter loading, and seasonal transitions. Equipment sized solely for peak conditions may cycle excessively or lose control authority at low loads.
A useful load schedule distinguishes continuous moisture entry from intermittent disturbances. It should also show which moisture sources change when exhaust flows or pressure relationships change.
Hypothetical example: A wafer-processing bay with variable exhaust could need different makeup-air treatment during standby than production, despite unchanged room dimensions and equipment layout.
Compare Technologies Against Required Supply Conditions
Refrigerant and Cooling-Coil Dehumidification
Cooling-based systems remove water by bringing air below its dew point and draining condensed moisture. They are practical when coil temperatures and available cooling can meet required supply conditions.
Performance depends on entering-air temperature and humidity, airflow, coil conditions, and defrost behavior. Very low requested dew points can introduce icing, reheating, or impractical operating conditions.
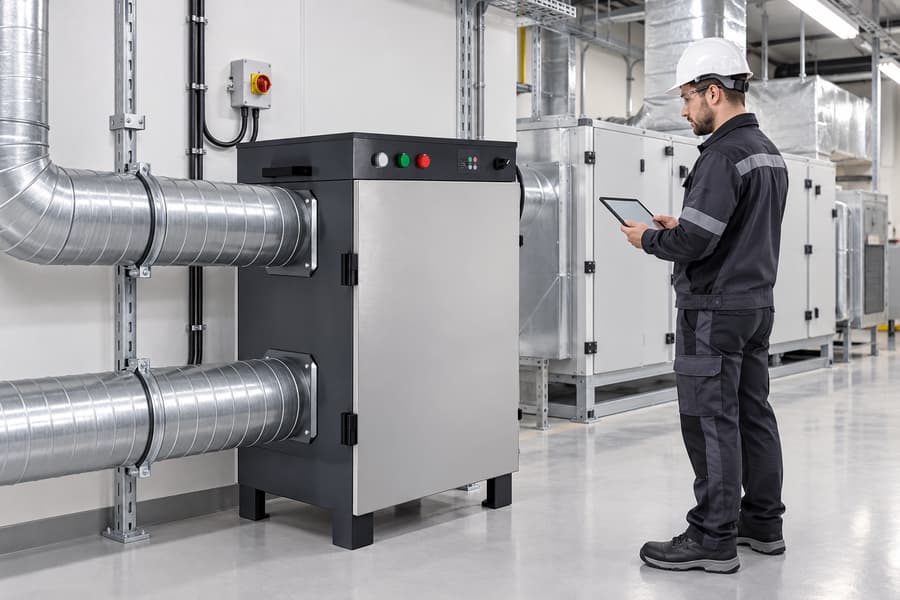
Review WetWells industrial dehumidifier configurations as potential equipment approaches, not proof of semiconductor cleanroom suitability. Installation-specific performance and contamination controls require separate engineering review.
Desiccant Systems for Lower Moisture Conditions
Desiccant rotors transfer water vapor from process air to a regeneration stream. They can serve lower dew-point duties when cooling condensation alone becomes limiting.
Compare process airflow, entering moisture, regeneration heat, leakage, purge requirements, and delivered air temperature. Rotor seals and downstream filtration deserve particular attention near sensitive manufacturing operations.
An advertised low-RH capability does not establish performance in a particular bay. Suppliers should provide leaving-air moisture data under the actual entering-air and regeneration conditions.
Hybrid arrangements can use cooling for bulk moisture removal and desiccant treatment for final drying. Compare their combined controls and regeneration demands against separate alternatives.
When Both Humidification and Dehumidification Are Needed
Cold or strongly dried makeup air can push some zones below their specified lower limit. In those cases, humidification may be necessary alongside moisture removal.
Consider water purity, aerosol generation, microbial management, wetted components, and downstream filtration. A humidifier acceptable in ordinary HVAC service may require redesign or exclusion from critical air paths.
A WetWells humidifier-dehumidifier combination can frame discussions about two-way control and integration. Actual suitability depends on approved humidification method, cleanliness requirements, and tested operating sequences.
Decide Between Central, Zoned, and Local Systems
Match Architecture to the Moisture Boundary
Central treatment at the makeup-air unit may efficiently address imported water vapor before air reaches production zones. It cannot automatically guarantee identical conditions at distant tools.
Independent zones become valuable when process limits, heat loads, operating schedules, or disturbances differ. They add control flexibility but also require more sensors, interfaces, and maintenance coordination.
Dedicated enclosures or dry cabinets can protect especially sensitive materials without drying an entire bay to the same condition. Their access patterns and leakage rates govern achievable recovery.
Avoid Unnecessary Equipment Duplication
Select the smallest defensible control boundary that contains the risk. A separate dehumidifier in every room can create competing loops and unpredictable pressure changes.
Conversely, one central system may leave a critical operation exposed during maintenance or supply-air disturbances. Compare architectures using consequence of failure, not equipment count alone.
Specify Capacity, Sensors, and Control Accuracy
Request Ratings at Project Conditions
Supplier capacity tables often reflect defined laboratory inlet conditions, airflow, and power arrangements. Moisture removal and achievable leaving-air conditions change when these assumptions change.
Request performance curves or selected-point calculations covering humid, dry, and part-load conditions. Include process airflow, static pressure, thermal output, condensate handling, and regeneration utilities where applicable.
Evaluate fan capacity after adding duct resistance and filtration. A unit meeting nominal moisture capacity without delivering required airflow may fail the installed application.
Separate Display Resolution From Measurement Uncertainty
A display showing small RH increments does not establish equivalent accuracy. Consider sensor calibration uncertainty, drift, temperature influence, installation location, and data acquisition errors together.
Match the total measurement uncertainty to the permitted process band and alarm margins. Specify calibration intervals, traceability, access for verification, and procedures for failed or suspect sensors.
Do not equate controller setpoint resolution with whole-room control accuracy. Spatial gradients, air mixing, actuator limits, and disturbances must be included in performance acceptance.
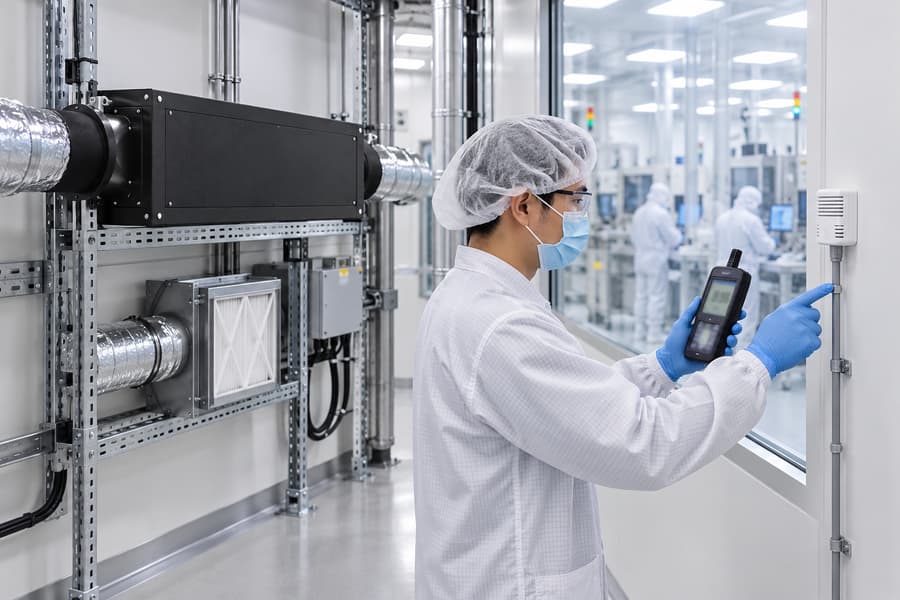
Monitor RH and temperature at critical fabrication-area locations, including process zones and air-handling equipment. Select measurement positions to represent the conditions that the system needs to control.
Select Sensor Locations That Represent the Risk
Place primary control sensors away from direct supply jets, open doors, and local heat sources unless those positions represent the product exposure of concern.
Use additional monitoring points for room mapping, cabinet access, or critical-tool locations. Independent witness sensors help distinguish actual humidity excursions from control-sensor failure.
Protect Cleanroom Airflow, Surfaces, and Materials
Preserve Filtration and Pressure Relationships
Any added unit must fit the facility’s cleanroom air-distribution strategy. Verify supply and return paths, filtration interfaces, pressure cascade, and exhaust replacement before approving modifications.
A local unit discharging dry air can create short circuits or disturb sensitive zones. Consider how supply velocity and return locations affect sensor readings and environmental uniformity.
Evaluate Contamination From the Treatment Equipment
Review particle shedding, lubricant exposure, wetted surfaces, seal wear, construction materials, and maintenance activities. Desiccant carryover and downstream filtration need explicit assessment rather than assumption.
Coils, drain pans, humidifier water systems, and duct insulation also introduce cleaning and contamination questions. Locate service-intensive components outside critical spaces where the design permits.
Check Dew Point Against Cold Surfaces
Condensation risk depends on local air dew point and surface temperature, not only the displayed room RH. Examine cold piping, equipment housings, and transient operating conditions.
Specify a project-defined condensation margin and verify it during challenging conditions. A satisfactory bay reading cannot justify omitting pipe insulation, sealed vapor barriers, or a properly detailed condensate route.
Build Stable Control and Failure Responses
Coordinate Dehumidification, Reheat, and Humidification
Define which controller owns the humidity target and which equipment responds first. Competing loops can cause simultaneous drying and humidifying or excessive cooling followed by reheat.
Set changeover logic, deadbands, minimum run times, and anti-windup behavior to suit process limits. Commission these sequences under both humid and dry conditions.
Separate normal control adjustments from alarms requiring operator action. Trend temperature, RH, dew point when relevant, equipment states, and valve or heater outputs to explain deviations.
Address Electrostatic and Operational Risks Separately
Humidity can affect charging behavior, but it must not replace qualified grounding, ionization, packaging, and materials controls. The ESD Association’s humidity guidance states humidity control is not an ANSI/ESD S20.20 requirement.
If a facility’s ESD control plan specifies humidity, define monitoring and responses to excursions. Verify ESD protection independently across the environmental conditions actually experienced.
Evaluate redundancy according to product exposure, permissible downtime, and recovery time. Standby equipment is justified by a documented failure consequence, not by a universal semiconductor rule.
Define the safe response when utilities fail or redundancy cannot recover the specified environment. Operational holds may be more appropriate than promising uninterrupted conditions.
Evaluate Installation, Energy, and Maintainability
Compare Full-System Energy Rather Than Nameplate Power
Include cooling, reheat, fans, humidification, regeneration heat, pumps, and controls when comparing alternatives. Energy intensity changes with weather, load, and operating sequence.
Assess heat-recovery opportunities without compromising cleanliness or exhaust isolation. An apparently efficient dehumidifier can create larger upstream or downstream loads if temperature control is poorly coordinated.
Plan Service Access and Utilities Early
Confirm electrical supply, cooling connections, drainage, safe condensate routing, regeneration exhaust, filter replacement space, and calibration access. Verify structural and vibration constraints near sensitive instruments.
Prevent maintenance work from exposing cleanroom air paths unnecessarily. Document isolation arrangements, cleaning procedures, consumables, spare parts, and procedures for returning equipment to validated operation.
Commission the System and Demonstrate Zone Performance
Use Factory Tests to Reduce Installation Risk
Factory acceptance testing (FAT) should confirm submitted configurations, controls, alarms, relevant airflow and moisture-removal functions, and agreed performance conditions that can actually be reproduced.
Factory testing cannot prove installed room uniformity or the effect of connected cleanroom airflows. Record test boundaries and open issues before equipment shipment.
Conduct Site Testing Across Operating Modes
Site acceptance testing (SAT) should verify airflow balance, pressure relationships, sensor calibration, drainage, utilities, and communication with the facility monitoring system.
Map RH and temperature at representative locations under agreed production, idle, and transition scenarios. Test access disturbances and recovery where they matter to material handling.
Document sensor placement, data intervals, measurement uncertainty, and acceptance calculations before testing. Otherwise, different teams can interpret the same environmental trend as passing or failing.
Validate control behavior at changeover between drying and humidifying, and during sensor faults or equipment shutdowns. Compare recorded excursions against the approved process response rules.
| Acceptance stage | Practical test | Evidence to retain |
| FAT | Controls, alarms, configured equipment and reproducible duty points | Signed results and exceptions |
| SAT | Airflow, utilities, drainage, pressure cascade, BMS interfaces | As-built checks and trend logs |
| Environmental mapping | Spatial RH/temperature variation under agreed modes | Sensor map and calibrated records |
| Disturbance and fault tests | Access recovery, mode changeover, alarms, standby response | Time histories and corrective actions |
Establish an Ongoing Verification Routine
Hand over baseline trends, alarm limits, calibration plans, filter and rotor service instructions, and clear ownership of changes. Include a procedure for investigating unexplained humidity excursions.
Recheck performance after tool additions, exhaust changes, airflow rebalancing, sensor replacement, or control software updates. Recalculate the affected moisture loads whenever the revised arrangement differs from the basis used during initial selection.
Prepare Procurement Specifications That Can Be Tested
Give Suppliers a Complete Duty Schedule
Issue room and enclosure limits, design temperatures, airflow schedules, outdoor-air conditions, latent loads, utilities, contamination constraints, and required monitoring locations with each request for quotation.
Require bidders to identify assumptions, operating boundaries, exclusions, and performance at specified conditions. Ask which components need site integration and which verification tasks remain with the facility.
Make Acceptance Criteria Contractual
Use the agreed specification to define measurable deliverables before purchase. Separate equipment duty guarantees, conditional on stated test conditions, from building-wide performance responsibilities.
- Technical submittals: Capacity selection, psychrometric basis, pressure drops, materials, filtration, utilities, and expected operating modes.
- Controls package: Sensor schedule, sequence of operation, alarms, data points, changeover logic, and fault responses.
- Test package: FAT and SAT procedures, environmental mapping plan, calibration records, and explicit pass/fail criteria.
- Handover package: As-built drawings, maintenance access, spare parts, training, baseline trends, and responsibility for corrective work.
Resolve gaps between supplier scope and facility scope before award. During commissioning, close deviations with dated evidence and process-owner approval before releasing critical areas for production.